When microbial counts repeatedly exceed your limits, food factory air disinfection is one area worth reviewing. A food processing facility may clean equipment every day and perform ozone disinfection after each shift, yet environmental monitoring results can still remain inconsistent. In many cases, the issue is not simply whether the factory disinfects, but whether the air is being controlled throughout the entire production cycle.
1. Disinfection Is Only Performed After Production
A common sanitation routine is simple:
Production → cleaning → ozone disinfection → shutdown
This can be useful for reducing environmental contamination after production. But it does not control what happens during the several hours between startup and shutdown.
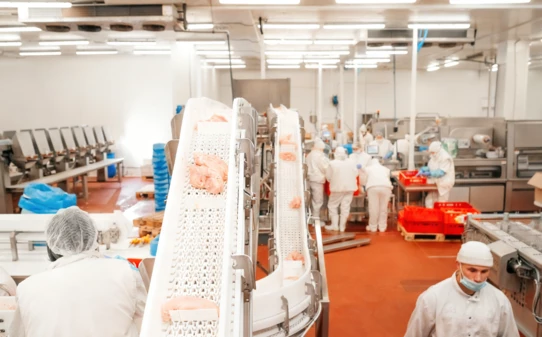
During production, workers move through the facility, raw materials and packaging materials are transferred, doors are opened, equipment operates, and air is continuously circulated.
All of these activities can influence the airborne microbial load.
This becomes particularly important in areas where products are exposed after cooking, cooling, cutting, filling, or before final packaging.
The problem with “disinfect once at the end of the day”
Overnight disinfection creates a relatively clean starting point, but production itself can introduce new contaminants.
That means there are actually two different sanitation questions:
What happens after production?
and
What happens while people are working?
A complete environmental hygiene strategy needs to consider both.
For occupied production areas, appropriately designed germicidal UV systems can provide continuous air treatment without directly exposing workers to UV-C radiation. CDC/NIOSH notes that GUV systems can be installed inside air-handling systems or in specially designed fixtures for occupied spaces.
The important point is not simply “use UV”.
The system must be correctly designed, installed, maintained, and operated.
2. Ozone Concentration Is Not Simply “Higher Is Better”
Ozone is widely used for disinfection because of its strong oxidation properties.
However, ozone is also a substance that requires strict control when people may be exposed to it.
For example, OSHA lists an 8-hour permissible exposure limit of 0.1 ppm (0.2 mg/m³) for ozone in the workplace.
This is why ozone disinfection normally belongs in an unoccupied period, with appropriate controls before workers re-enter the treated area.
Using too little ozone may result in insufficient treatment under the specific conditions.
Using excessive ozone can create other problems:
- Longer waiting time before personnel can enter
- Greater occupational exposure concerns
- Potential material compatibility issues
- More complicated ventilation and residual-gas management
- Disruption to production schedules
Ozone performance also depends on the actual application conditions. Room volume, temperature, humidity, air movement, treatment time, and the target microorganisms all matter.
So the real question is not:
“How much ozone can we use?”
It is:
“What treatment level and exposure time are appropriate for this application?”
This is an important distinction when designing an industrial food factory air disinfection system.
3. One Disinfection Method Cannot Cover Every Production Stage
Another common problem is using the same disinfection method throughout the entire production cycle.
But the conditions are different:
During production:
Workers are present, products may be exposed, and continuous air treatment may be required.
After production:
The area is empty, allowing stronger treatment methods such as ozone to be considered under controlled conditions.
This is why a two-stage air disinfection strategy can make more sense for some food processing facilities:
During production: UV air treatment
Air is continuously drawn into the equipment and exposed to UV-C inside a shielded disinfection chamber.
The UV source is enclosed inside the unit rather than directly irradiating the production area.
When properly designed and maintained, enclosed or duct-based UV systems can treat recirculated air while minimizing direct UV exposure to people. CDC describes this type of application as a supplemental air-cleaning measure.
After production: Ozone treatment
Once personnel have left the production area, ozone can be used as part of the facility’s post-production sanitation procedure.
The system should be operated according to the equipment design, site conditions, applicable safety requirements, and the manufacturer’s instructions.
Before personnel return, the area needs to meet the facility’s established safety and re-entry requirements.
This creates a practical operating concept:
UV during production → Ozone after production
Instead of relying on one method for every situation, the facility can use different technologies according to the production stage.
What Should Food Factories Check When Microbial Counts Stay High?
If environmental monitoring results repeatedly exceed your internal limits, don’t immediately assume that the solution is simply “more disinfectant”.
Start with the whole contamination-control chain.
1. Check the sampling locations
Are the sampling points located close to exposed products, cooling areas, packaging lines, personnel traffic routes, or other high-risk zones?
2. Check production-time contamination
Look at what happens during production, not only after cleaning.
Personnel movement, doors, material transfer, airflow patterns, and equipment operation can all influence the environment.
3. Check ventilation and air movement
Air disinfection works together with ventilation and filtration.
CDC/NIOSH recommends considering filtration and GUV as components of broader indoor air-cleaning strategies, rather than treating GUV as a replacement for required ventilation or filtration.
4. Check UV system performance
A UV lamp being switched on does not automatically mean that effective UV treatment is being delivered.
Lamp condition, airflow, exposure time, chamber design, cleanliness, and maintenance all matter.
CDC notes that UV systems require appropriate design and regular maintenance, including keeping lamps clean and replacing aging lamps as required.
5. Check ozone operation
Review the actual treatment time, room volume, ozone concentration, ventilation, and re-entry procedure.
Ozone should never be treated as an ordinary “air freshener” or run around personnel without appropriate safety controls.
A More Practical Approach to Food Factory Air Disinfection
For many food processing facilities, air disinfection should be viewed as one layer of environmental hygiene, not a standalone solution.
A practical strategy may look like this:
| Production stage | Typical objective | Possible approach |
|---|---|---|
| Before production | Establish a controlled environment | Cleaning + sanitation + ventilation |
| During production | Control airborne microbial load | Enclosed UV/GUV air treatment + ventilation/filtration |
| After production | Reduce environmental contamination | Ozone or other validated sanitation methods |
| Before next shift | Confirm safe re-entry | Ventilation + safety verification |
| Ongoing | Verify sanitation performance | Environmental monitoring and trend analysis |
The exact combination should be determined according to the facility layout, production process, risk level, regulatory requirements, and environmental monitoring results.
The key is to move from “disinfect once a day” to a more complete continuous contamination-control strategy.
How WONE Approaches Air Disinfection for Food Processing Facilities
WONE provides industrial hygiene equipment for food processing environments, including personnel hygiene, equipment cleaning and air disinfection.
For air treatment, WONE systems can combine different operating modes for different production stages.
UV Air Disinfection During Production
WONE UV air disinfection systems use an enclosed treatment chamber to expose recirculated air to UV-C inside the equipment.
This allows the unit to continuously treat air while production is running, when the system is properly installed and operated for occupied-space use.
Ozone Disinfection After Production
During unoccupied periods, ozone can be used for post-production environmental disinfection according to the selected system and site requirements.
The operating schedule can be programmed so that UV treatment and ozone treatment are used at different times.
Automatic Operation
For factories running multiple shifts, automated scheduling can reduce the need for operators to manually switch between different disinfection modes.
This can be particularly useful when air disinfection is integrated into a broader sanitation program.
The Bigger Picture: Air Disinfection Is Only One Part of Food Hygiene
Repeated microbial counts should never be treated as an air-disinfection problem alone.
FDA guidance emphasizes sanitary operations, personnel practices, sanitary equipment and environmental monitoring as parts of a broader microbial hazard-control system.
If microbial results remain high, investigate the complete process:
Personnel → Equipment → Surfaces → Air → Water → Drainage → Ventilation → Cleaning → Disinfection → Environmental Monitoring
Air treatment can help reduce airborne microbial contamination, but it works best as part of a layered hygiene strategy.
For food factories dealing with repeated environmental monitoring issues, the more useful question may not be:
“Which disinfectant should we use?”
It may be:
“Where is contamination entering the process, when is it increasing, and how can we control it continuously?”
That shift in thinking can make air disinfection a much more useful part of a food factory’s overall hygiene program.
Looking for an air disinfection system for a food processing facility?
WONE provides industrial hygiene equipment for food factories, including personnel hygiene systems, equipment cleaning systems and air disinfection equipment.
Contact WONE to discuss your production area, room size, process and hygiene requirements.